Overview
Summary
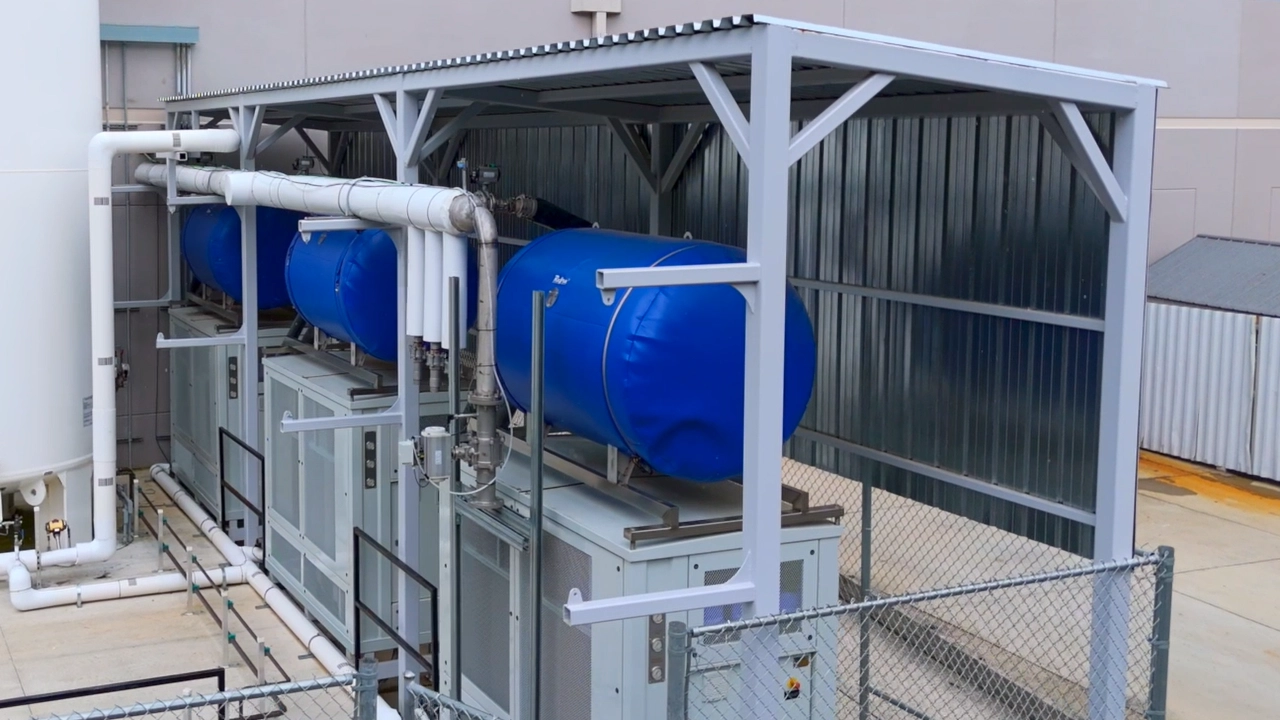
A Cold Jet RE-CO2 recovery system captures the CO₂ gas that a dry ice pelletizer normally vents, cools and compresses it back into liquid, and pipes it straight to the pelletizer. Dry ice plants cut liquid CO₂ consumption by nearly half, lower costs by up to 40%, and make up to 70% more dry ice.
What is dry ice CO₂ recovery?
Dry ice CO₂ recovery is carbon capture inside a dry ice plant. When liquid CO₂ (LCO₂) is brought to atmospheric pressure in a pelletizer chamber, roughly half turns into CO₂ snow that is pressed into pellets — and the other half becomes gas that is typically vented to atmosphere. A Cold Jet RE-CO2 recovery system collects that revert gas from the pelletizer vent, cools and compresses it back into liquid CO₂, and sends it through a valve into the line that feeds the pelletizer. Because it is a closed loop, dry ice quality is unaffected, and the recovered CO₂ never goes back into the supplier's bulk tank. The result is a far better LCO₂-to-dry ice conversion ratio: less liquid CO₂ bought, fewer deliveries, more dry ice from every tonne, and less CO₂ released. Systems range from 80 to 3,500 kg/hr and work with Cold Jet and most other pelletizer brands.
Challenge
Stop venting half of every CO₂ delivery
In standard dry ice production, around half of the liquid CO₂ you buy leaves the pelletizer as gas and is vented to atmosphere. You pay for CO₂ you never sell, depend on more frequent liquid CO₂ deliveries, and release avoidable emissions. Cold Jet RE-CO2 recovery systems capture that gas and turn it back into dry ice, cutting liquid CO₂ consumption by nearly half.
Up to 70%
More Dry Ice
Up to 40%
LCO₂ Cost Savings
80–3,500 kg/hr
Recovery Capacity
≤12 Months
Typical ROI
Benefits
What are the benefits of dry ice CO₂ recovery?
Cut liquid CO₂ costs and make more dry ice
Cold Jet RE-CO2 recovery systems capture the CO₂ gas your pelletizer vents, reliquefy it, and return it to the pelletizer, so every liquid CO₂ delivery produces more dry ice.
Without recovery, roughly half of the liquid CO₂ you buy is vented to atmosphere — raising costs, increasing reliance on deliveries, and adding avoidable emissions. Recovery turns that waste back into product.
 Cost Savings
Use Half the Liquid CO₂
Around half of the liquid CO₂ entering a pelletizer is normally vented as gas. Recovering it cuts liquid CO₂ consumption by nearly half and annual CO₂ costs by up to 40% — freeing a significant share of your operating budget to reinvest in growth.
 Output
Make More Dry Ice
Customers using RE-CO₂ recovery systems have increased dry ice production by up to 70% using the same amount of liquid CO₂. Recovered CO₂ goes straight back to the pelletizer, so every delivery produces more saleable dry ice.
 Sustainability
Reduce Vented CO₂
Recovery recycles an already recycled product and greatly reduces the exhaust CO₂ vented from typical dry ice production. Lower emissions strengthen your ESG story and your brand with customers who care about carbon footprint.
 Supply Security
Fewer LCO₂ Deliveries
Needing less liquid CO₂ reduces your reliance on external deliveries, so a late tanker or a regional CO₂ shortage is less likely to stop production. Plants run more smoothly and reliably, with more headroom in every bulk tank fill.
 Quality
Same Dry Ice Quality
The recovery system is a closed loop, which eliminates the chance of contamination. Recovered CO₂ is the same high quality as the liquid CO₂ used in production, so your dry ice pellets and blocks meet the same standard as before.
 Integration
Works With Your Pelletizers
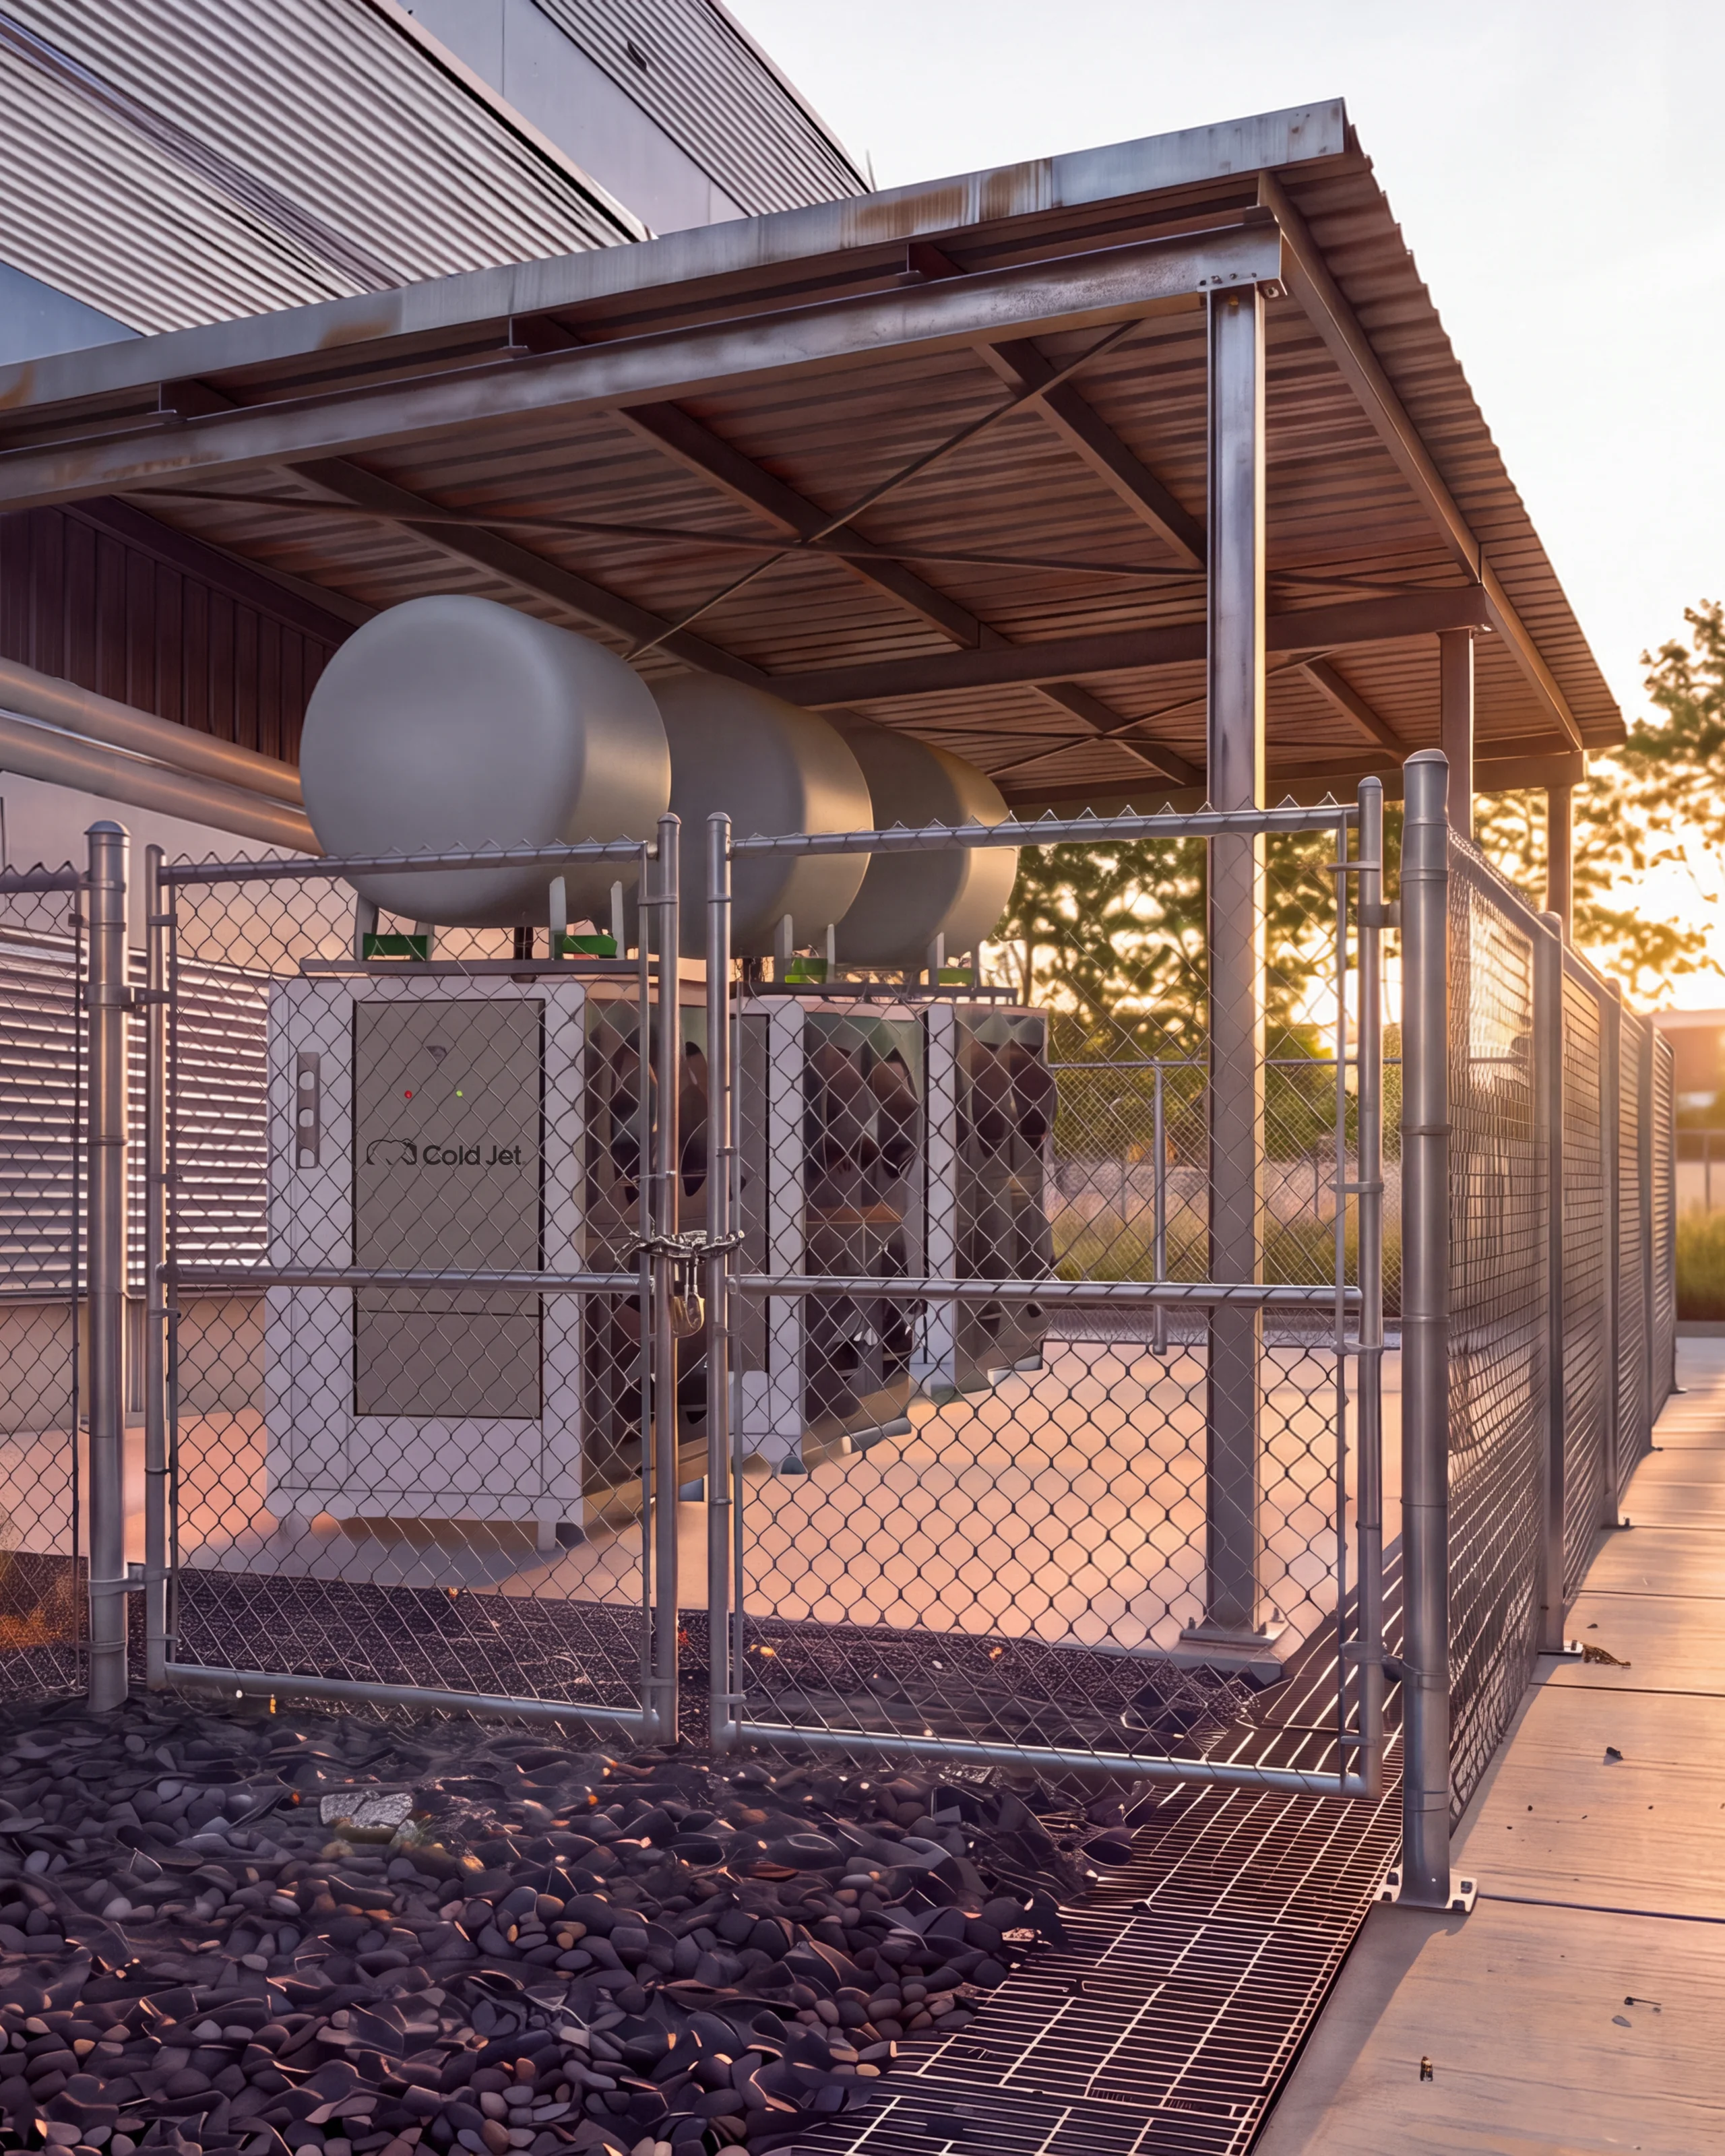
RE-CO2 systems integrate with all Cold Jet pelletizers, including Integrated Blasting Systems, and almost every other brand. Installation needs minimal extra equipment, and units can sit outside near the bulk tank when floor space is tight.
How It Works
How dry ice CO₂ recovery works
From capturing revert gas at the pelletizer vent to returning liquid CO₂ to the feed line — and sizing a system to your plant.
Validated For
- Dry Ice Production
- Pelletizer Revert Gas
- Closed-Loop Recovery
- Cold Jet Pelletizers
- Most Pelletizer Brands
- Integrated Blasting Systems
- Multi-Pelletizer Plants
- R744 Refrigerant (RE-CO2 3500)
How CO₂ recovery works
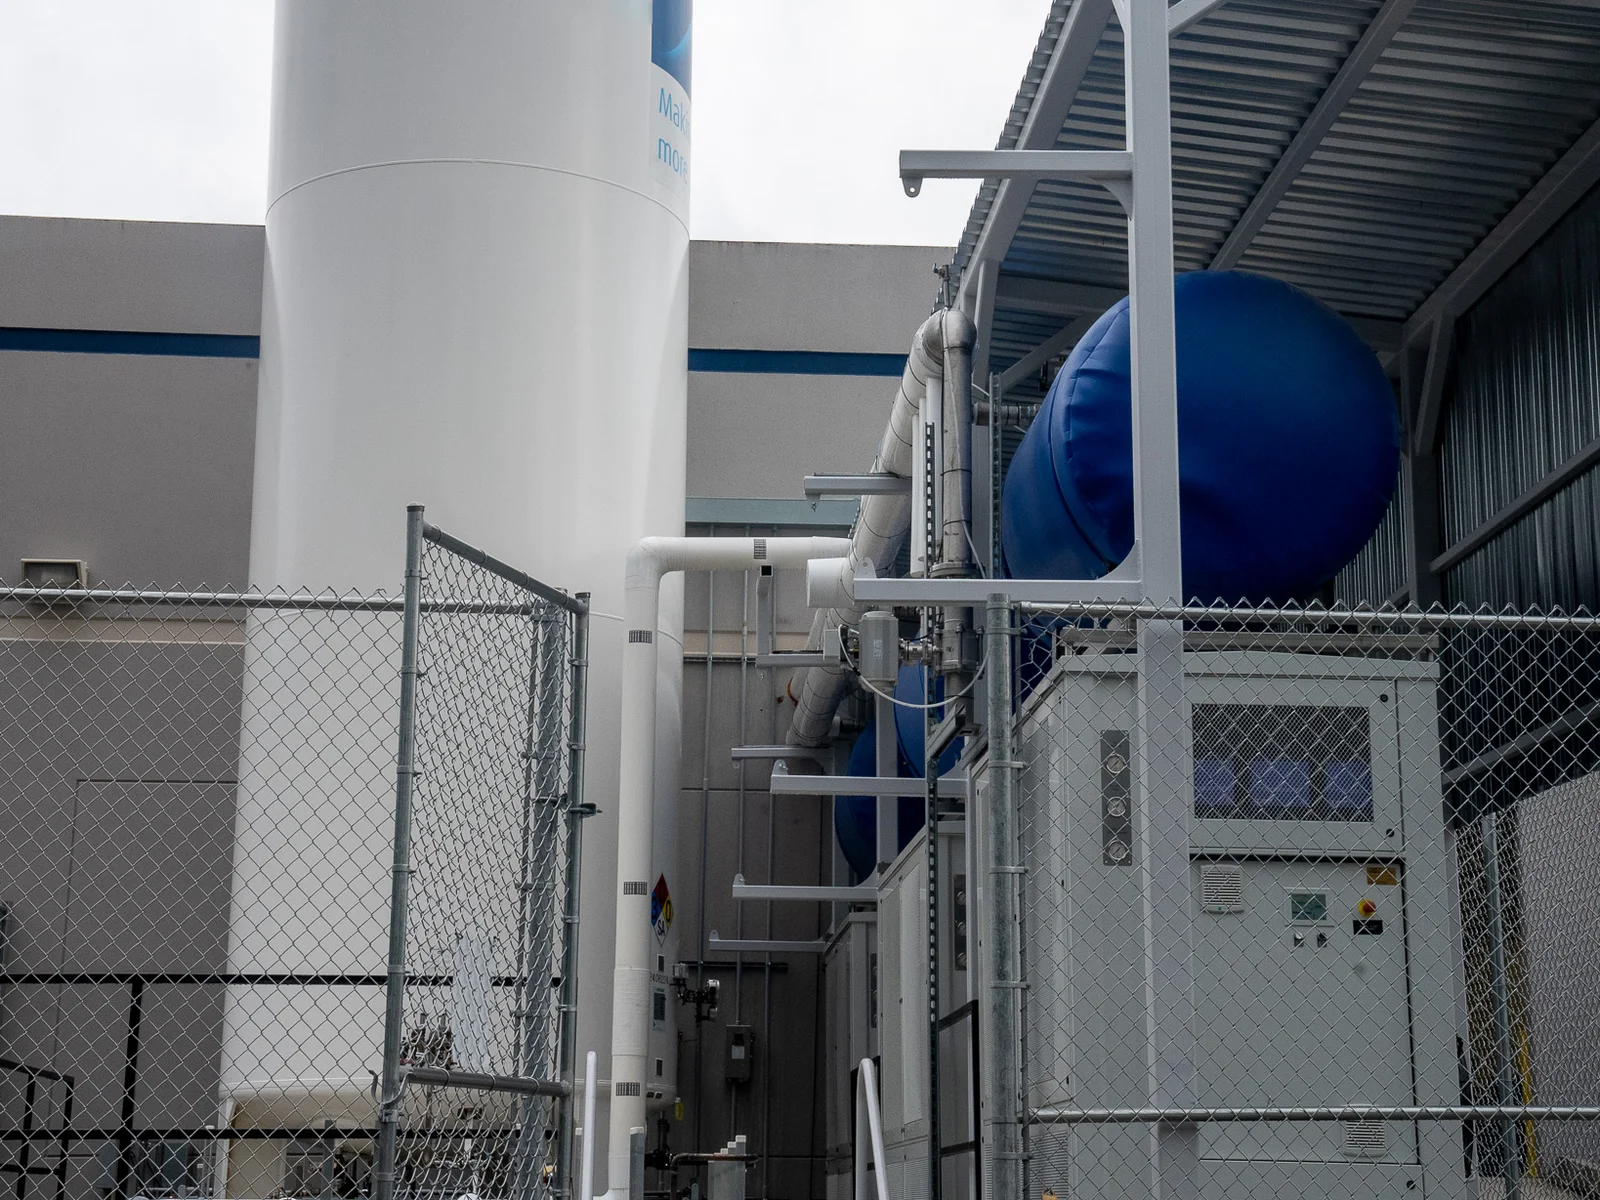
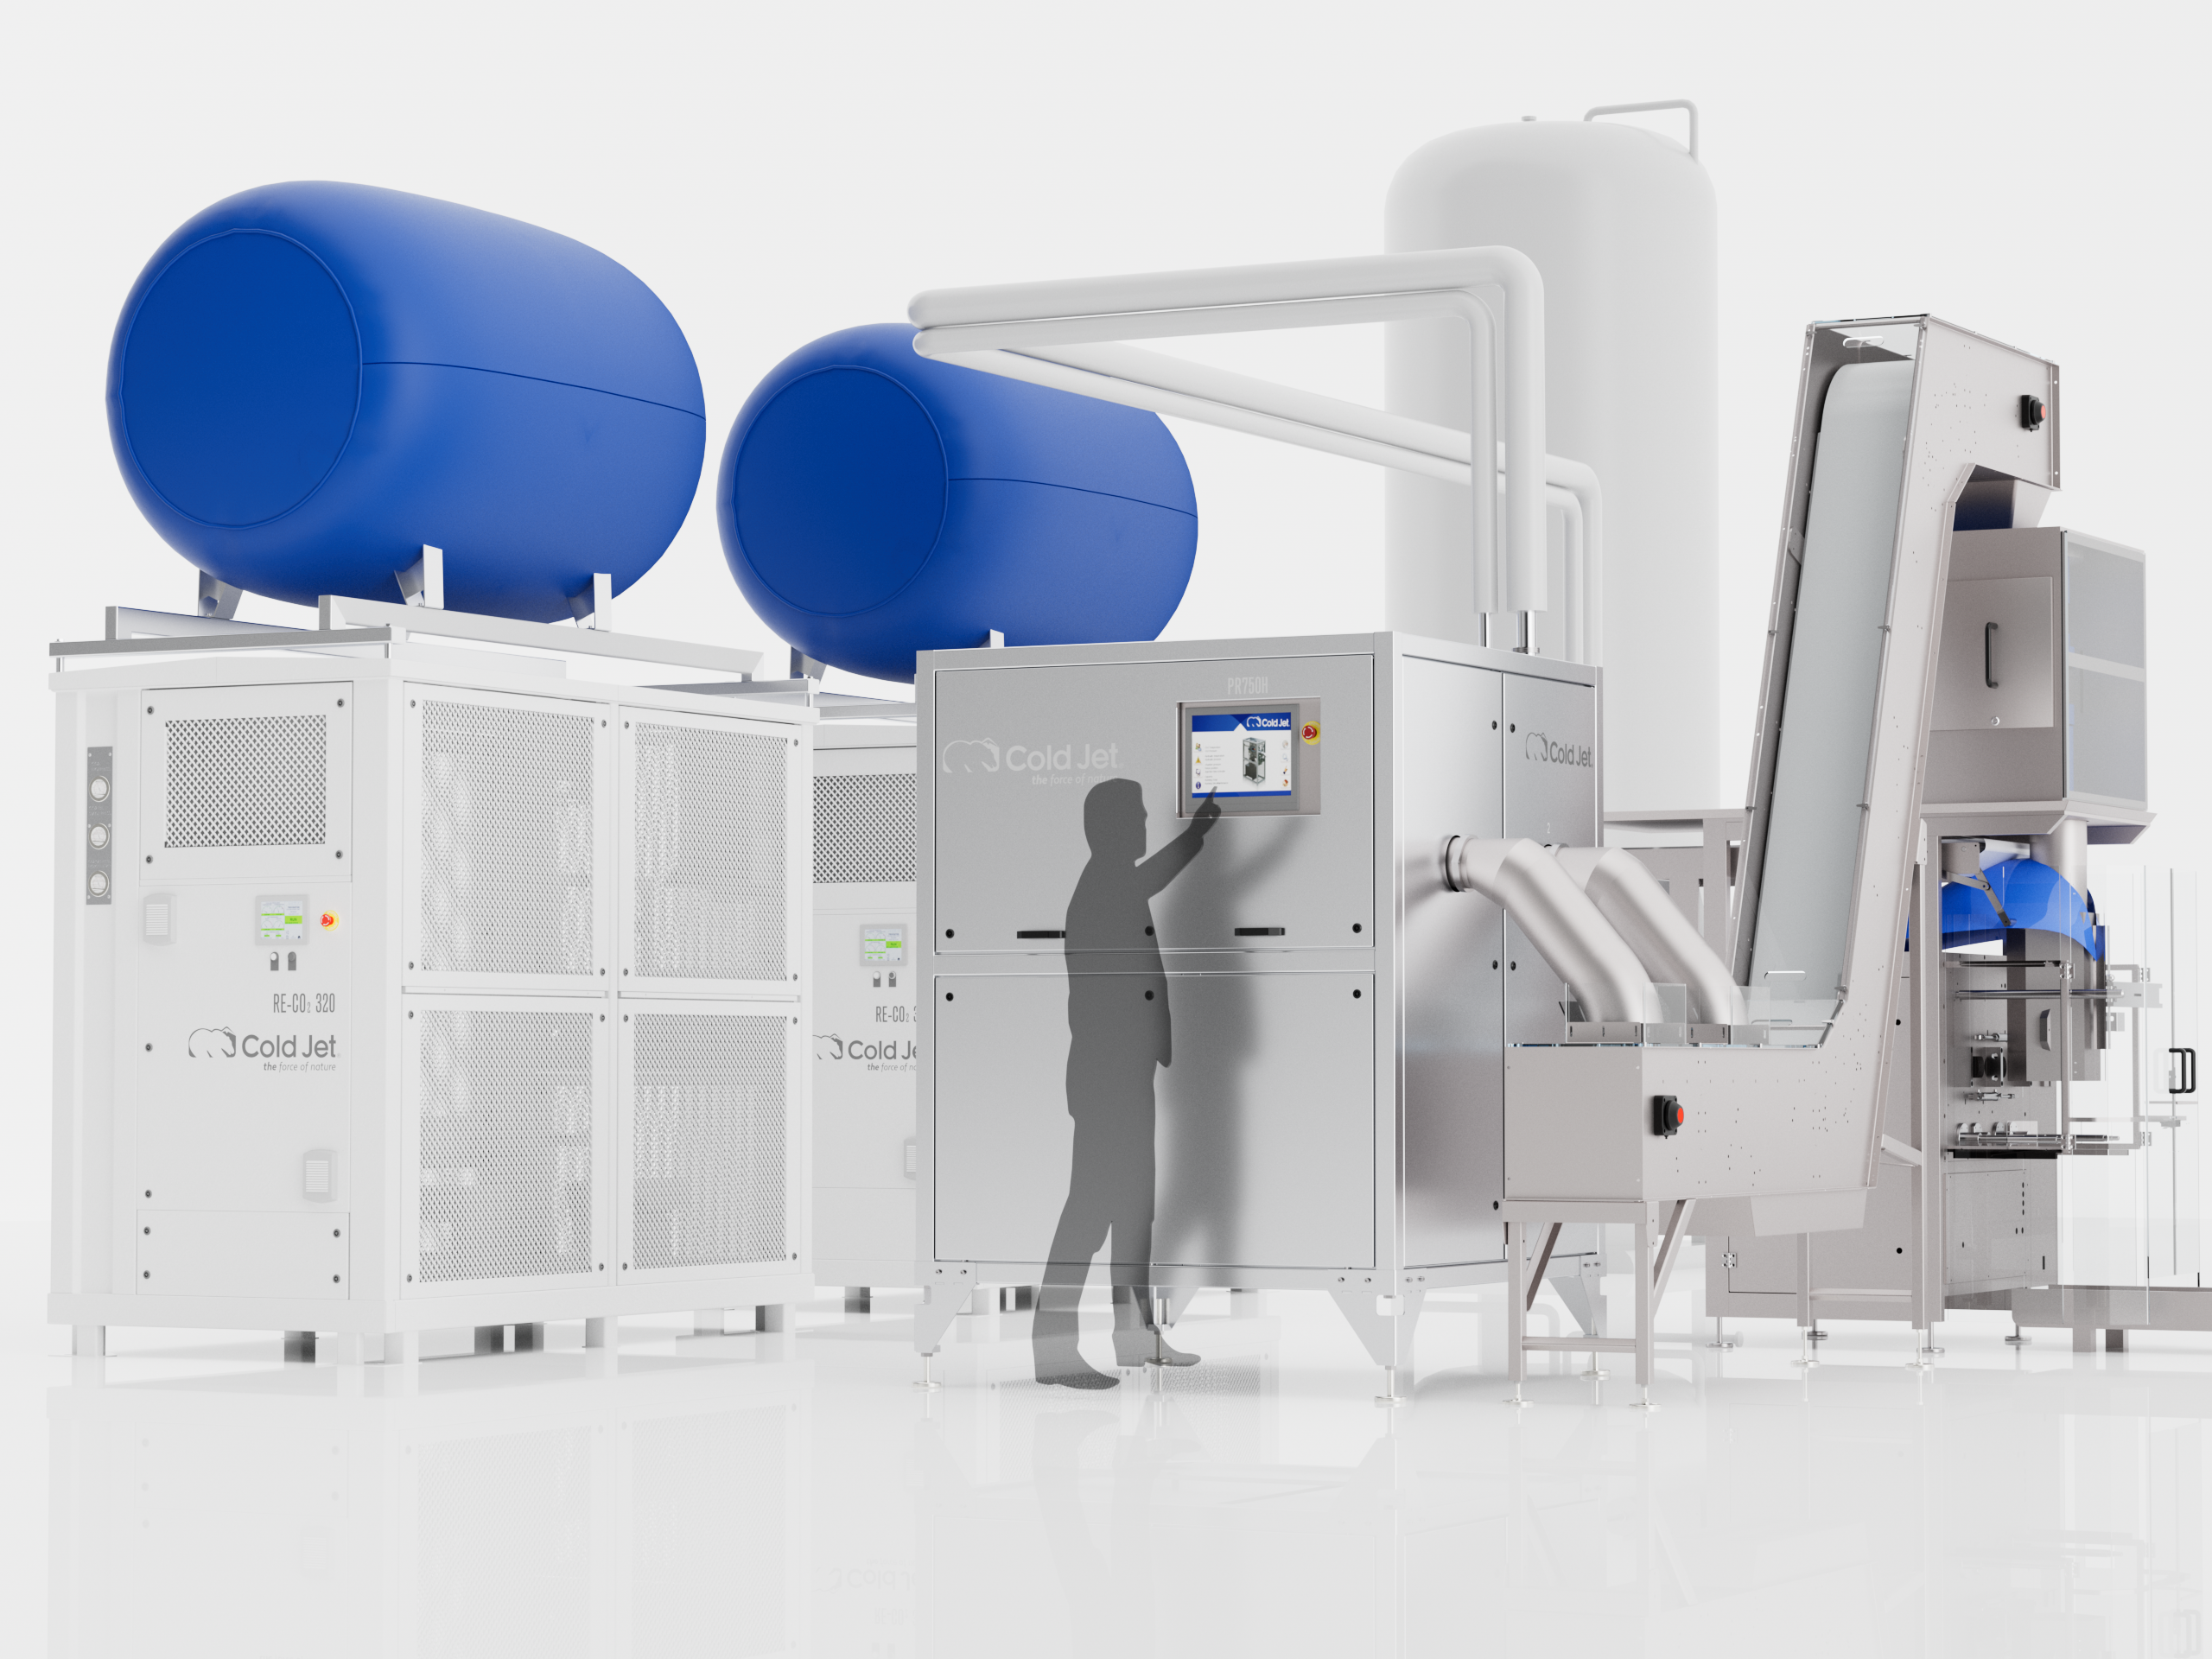
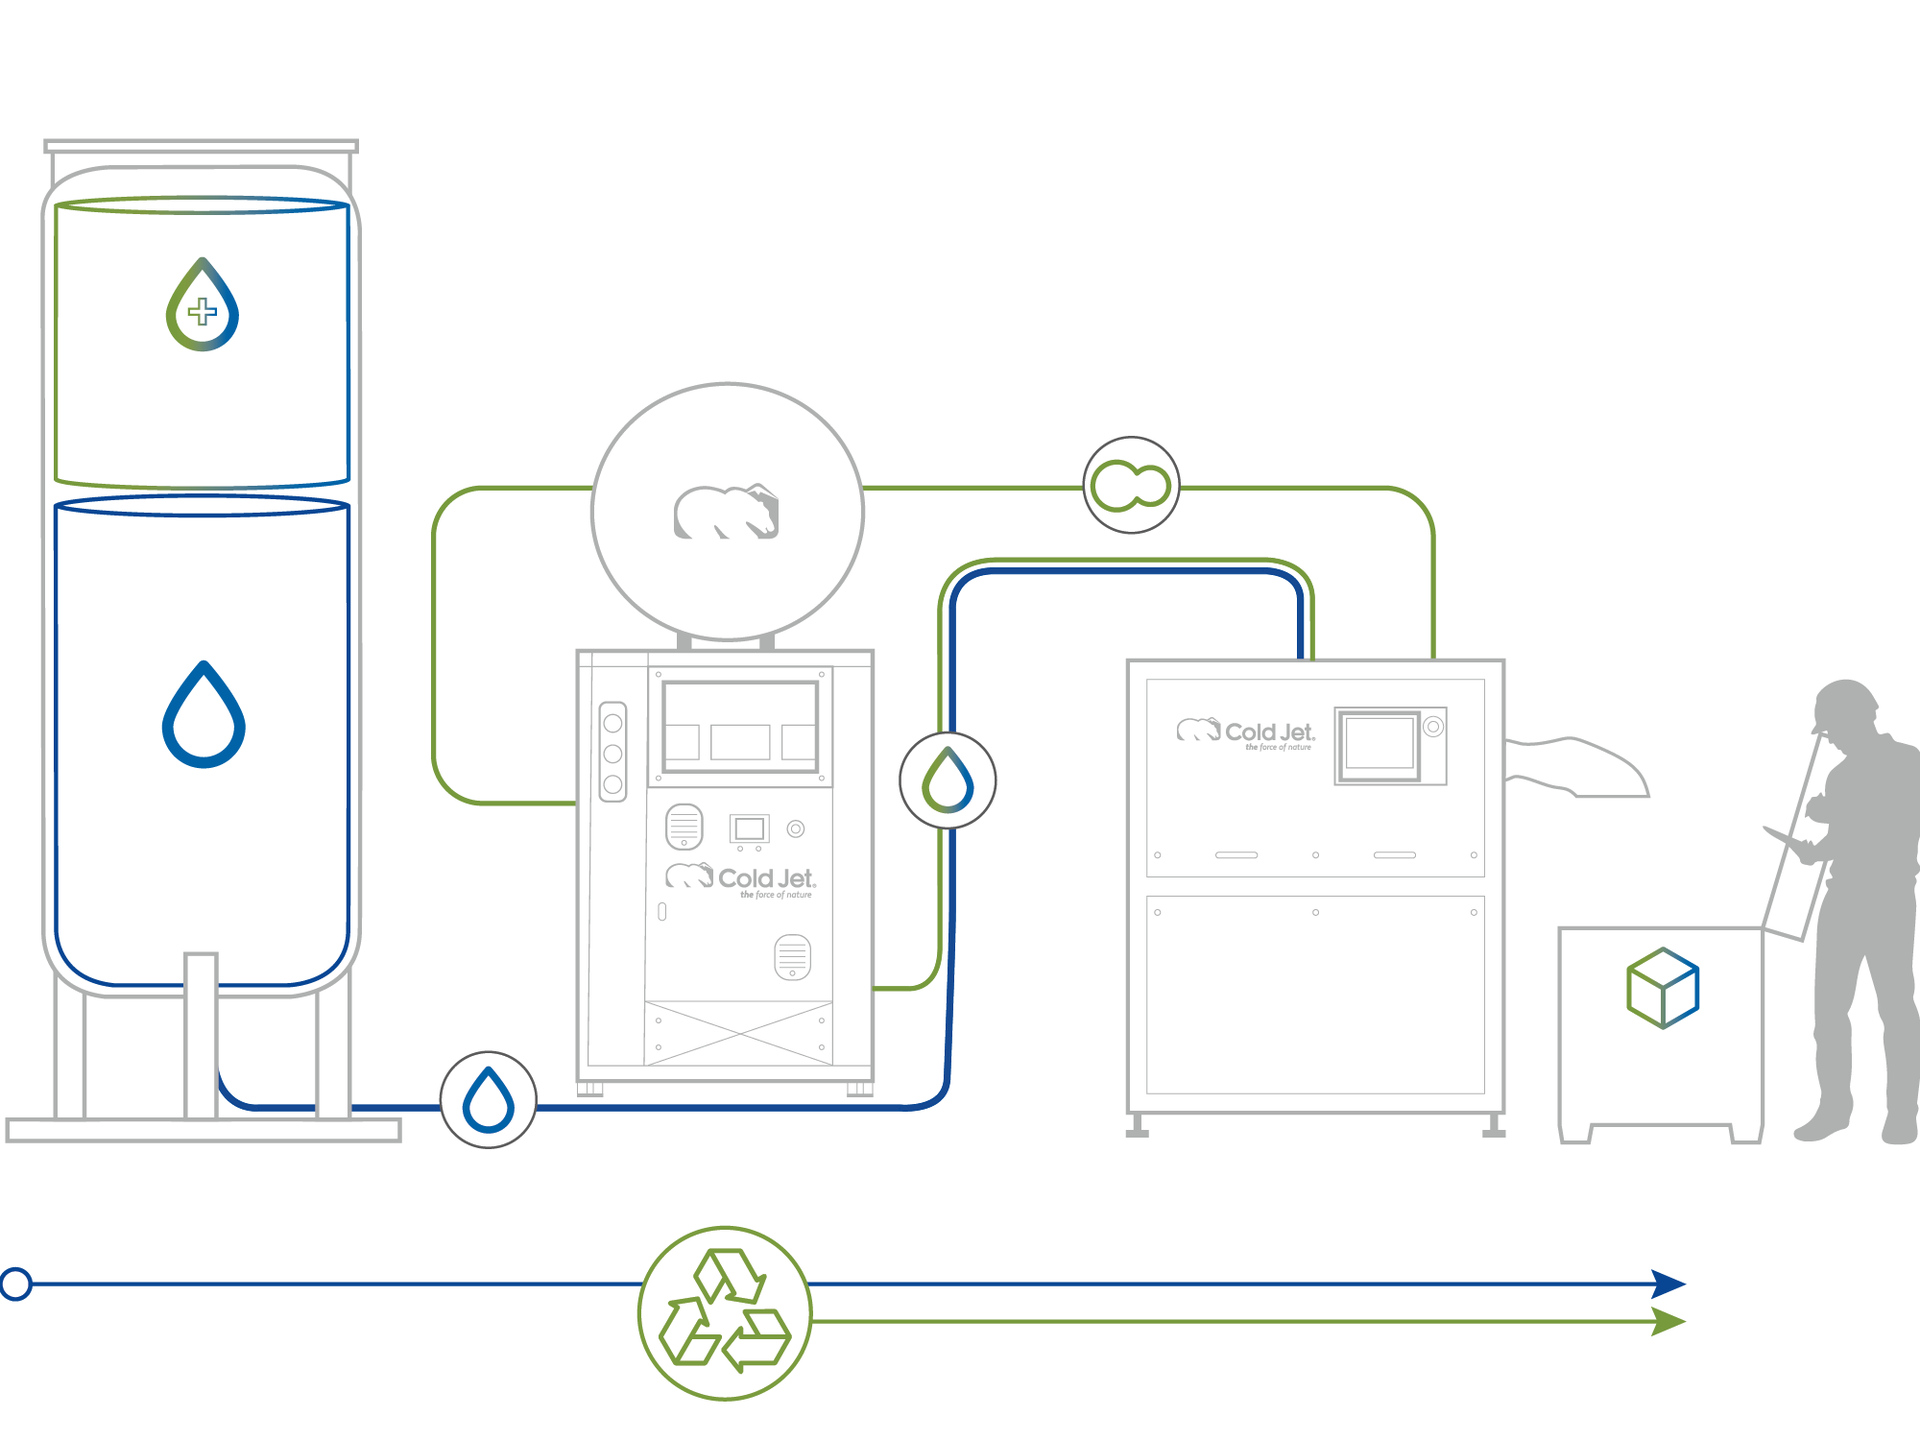
A RE-CO2 system sits between your pelletizer vent and its liquid CO₂ feed line. It captures the revert gas produced during pelletizing, reliquefies it, and returns it to the pelletizer to make more dry ice.
Capture at the pelletizer vent
When liquid CO₂ expands in the pelletizer chamber, about half becomes CO₂ snow and the other half becomes gas that would normally be vented. The recovery system collects that exhaust gas directly from the pelletizer vent through external hose connections, before it reaches atmosphere. Nothing changes about how the pelletizer itself produces dry ice.
Cool, compress and reliquefy
Inside the recovery unit, the gaseous CO₂ is cooled and compressed back into liquid CO₂. Energy use ranges from 298 kWh per tonne recovered on the RE-CO2 80 down to 135 kWh per tonne on the containerized RE-CO2 3500, which uses CO₂ (R744) as its refrigerant.
Return to the pelletizer, not the bulk tank
Recovered liquid CO₂ flows through a valve into the piping that feeds the pelletizer — never back into the bulk tank, which gas companies prohibit. The closed loop keeps quality identical and delivers a continuous flow of liquid CO₂, cutting LCO₂ consumption by nearly half in most installations.
System capabilities
- Revert Gas Capture
- CO₂ Reliquefaction
- Direct Pelletizer Feed
- Closed-Loop Operation
- Buffer Tank
- Pelletizer HMI Control
- Multi-Unit Gas Optimization
- Outdoor Installation Option
Recovery systems for every plant size
With a modular design and four liquefaction capacities, RE-CO2 systems scale from a single small pelletizer to high-volume plants. Start small and add capacity as efficiency and margins grow.
Small and mid-size production
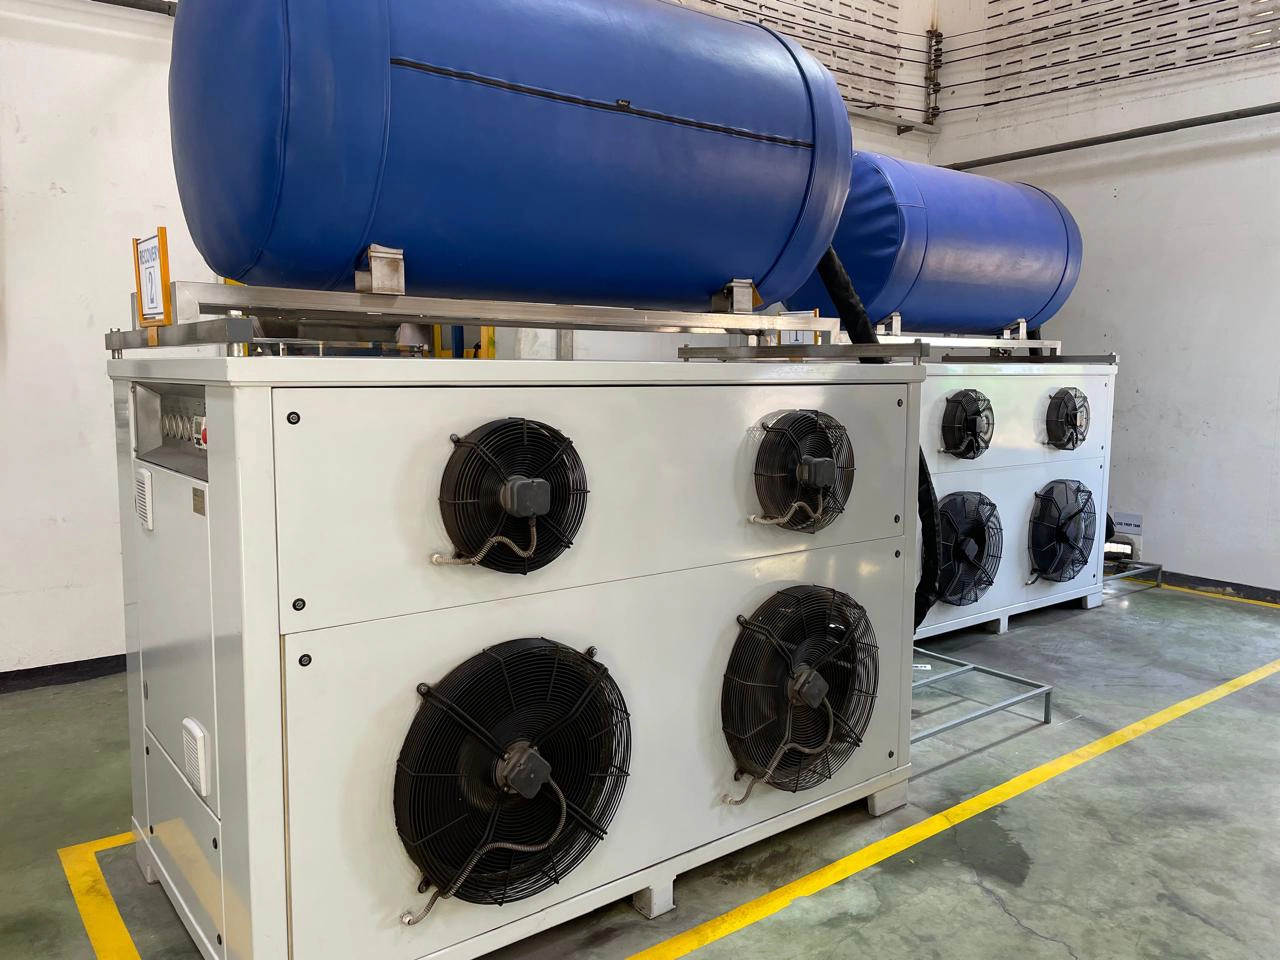
The RE-CO2 80 recovers up to 80 kg/hr and pairs with PE 80 pelletizers, the RE-CO2 160 recovers up to 160 kg/hr for PR120H pelletizers, and the RE-CO2 320V2 recovers up to 320 kg/hr for PR350H and PR750H pelletizers. The 320V2 starts and runs directly from your Cold Jet pelletizer's control panel.
High-volume dry ice plants
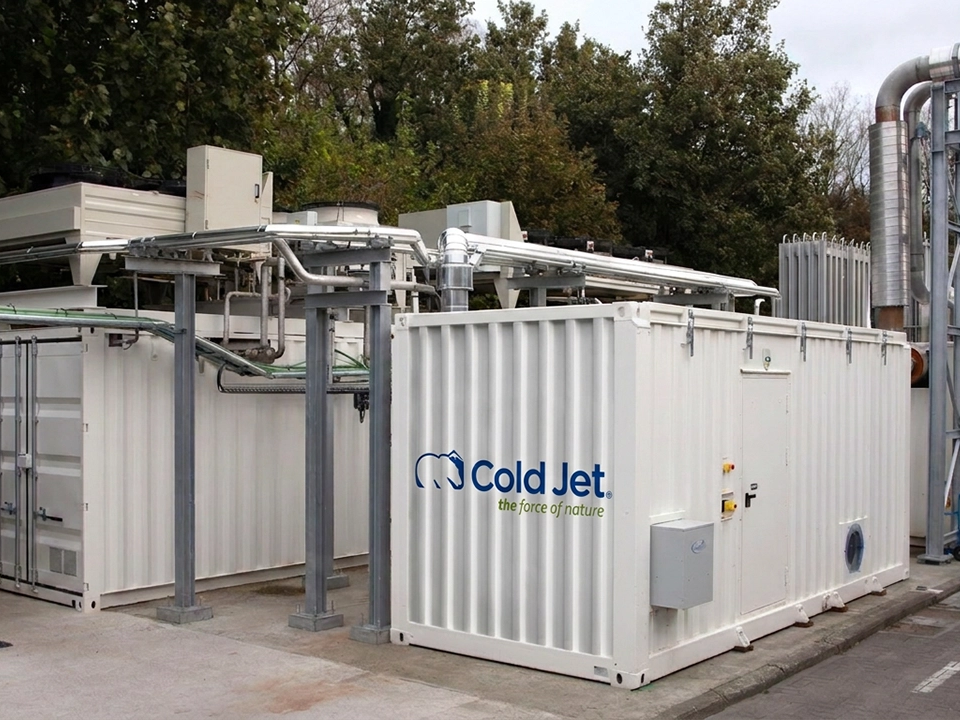
The RE-CO2 3500 recovers up to 3,500 kg/hr for plants running multiple PR750H pelletizers. It is autonomous and containerized, needs no extra building infrastructure, uses CO₂ (R744) as its refrigerant, and offers the lowest energy consumption per tonne recovered on the market. Custom platforms run from 1,200 to 5,000 kg/hr.
Integration with existing lines
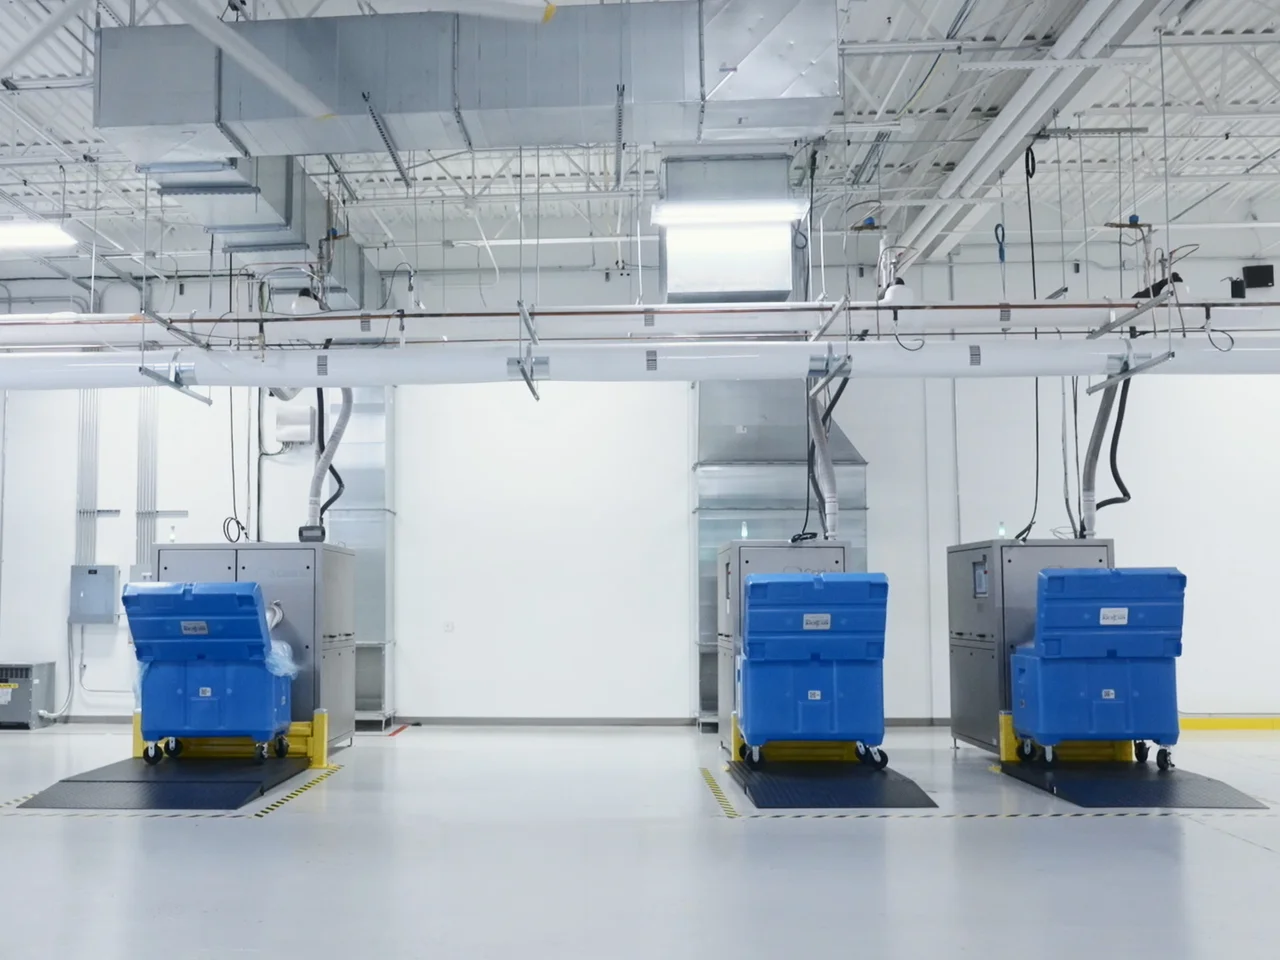
RE-CO2 systems are compatible with almost every pelletizer brand and with Cold Jet Integrated Blasting Systems. Where floor space is limited, units can be installed outside near the bulk liquid CO₂ tank, and Cold Jet helps plan the electrical supply.
RE-CO2 recovery systems pair with the following dry ice production equipment:
Compatible equipment
- PE 80 Pelletizers
- PR120H Pelletizers
- PR350H Pelletizers
- PR750H Pelletizers
- Multi-Pelletizer Plants
- Integrated Blasting Systems
- Most Competitor Pelletizers
Industries
Which Industries Use CO₂ Recovery for Dry Ice Production?
Whether you sell dry ice or make it for your own blasting, every pelletizer vents CO₂ you’ve already paid for. See how Cold Jet CO₂ recovery helps dry ice manufacturers make more product from every liquid CO₂ delivery.
Comparison
How CO₂ recovery
compares to venting
See how capturing pelletizer revert gas stacks up against standard dry ice production across the criteria that matter most.
| Criteria | RE-CO2 Recovery Best | Standard Production (Venting) |
|---|---|---|
| LCO₂ Consumption | Cut by nearly half | Baseline – about half vented |
| Dry Ice Output | Up to 70% more per LCO₂ | Baseline |
| CO₂ Costs | Up to 40% lower | Full cost of vented CO₂ |
| Vented CO₂ | Greatly reduced | About half of LCO₂ input |
| Delivery Reliance | Fewer LCO₂ deliveries | Higher – more tanker fills |
| Dry Ice Quality | Unchanged – closed loop | Standard |
What You Need
Dry ice CO₂ recovery: what equipment is needed?
A CO₂ recovery installation relies on several key components:
Step 01
RE-CO2 recovery system
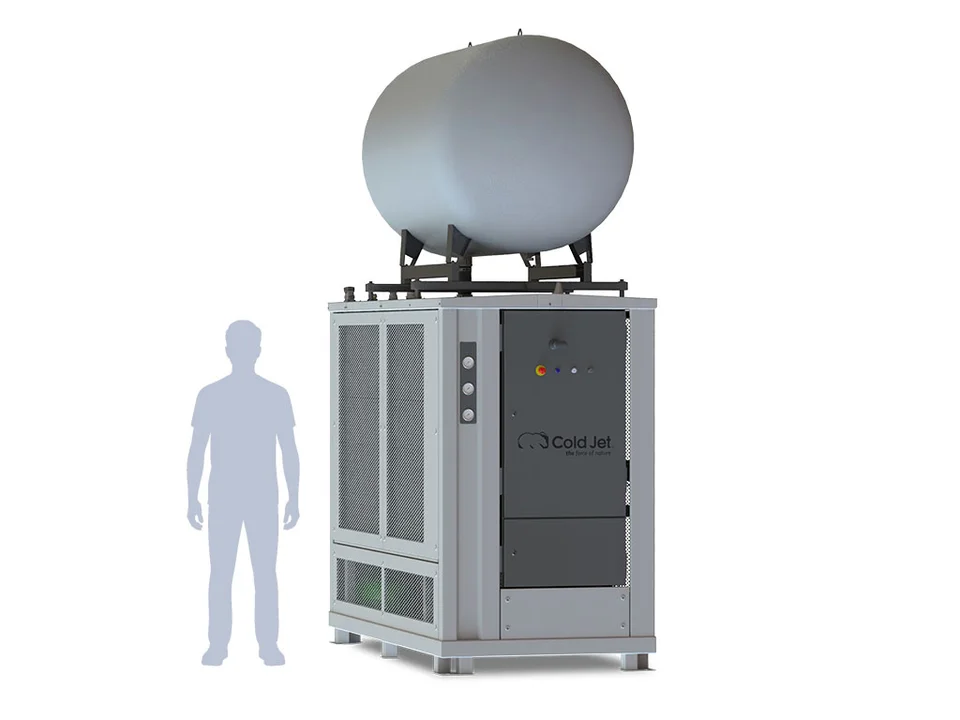
The core of the installation is a Cold Jet RE-CO2 recovery unit sized to your pelletizer output. Four capacities are available — 80, 160, 320 and 3,500 kg/hr — and the modular design lets you start small and add capacity later. Larger plants can have a custom platform configured from 1,200 to 5,000 kg/hr, with experts helping match the unit to your conversion goals.
- 01. RE-CO2 recovery system — The core of the installation is a Cold Jet RE-CO2 recovery unit sized to your pelletizer output. Four capacities are available — 80, 160, 320 and 3,500 kg/hr — and the modular design lets you start small and add capacity later. Larger plants can have a custom platform configured from 1,200 to 5,000 kg/hr, with experts helping match the unit to your conversion goals.
- 02. Dry ice pelletizer — RE-CO2 systems connect to your existing pelletizer — any Cold Jet model, Integrated Blasting Systems, and most competitor brands — with minimal modifications.
- 03. Gas connection and buffer tank — External hoses carry exhaust CO₂ gas from the pelletizer vent to the recovery unit, and recovered liquid feeds the pelletizer line. The RE-CO2 320V2 includes a buffer tank to optimize gas flow.
- 04. Electrical supply and site location — Recovery units install alongside your production equipment, or outside near the bulk liquid CO₂ tank if floor space is limited. Cold Jet helps you plan the electrical supply; the RE-CO2 320V2, for example, runs on 440–480 V AC at 60 Hz or 400 V AC at 50 Hz.
- 05. Controls and maintenance kits — Run the RE-CO2 320V2 from your Cold Jet pelletizer's HMI, add a line controller, and keep a spare parts kit and warm weather kit on hand.
Equipment
What is the best CO₂ recovery system
for dry ice production?
Dry ice producers choose from Cold Jet's RE-CO2 lineup to match their pelletizers and production volume.
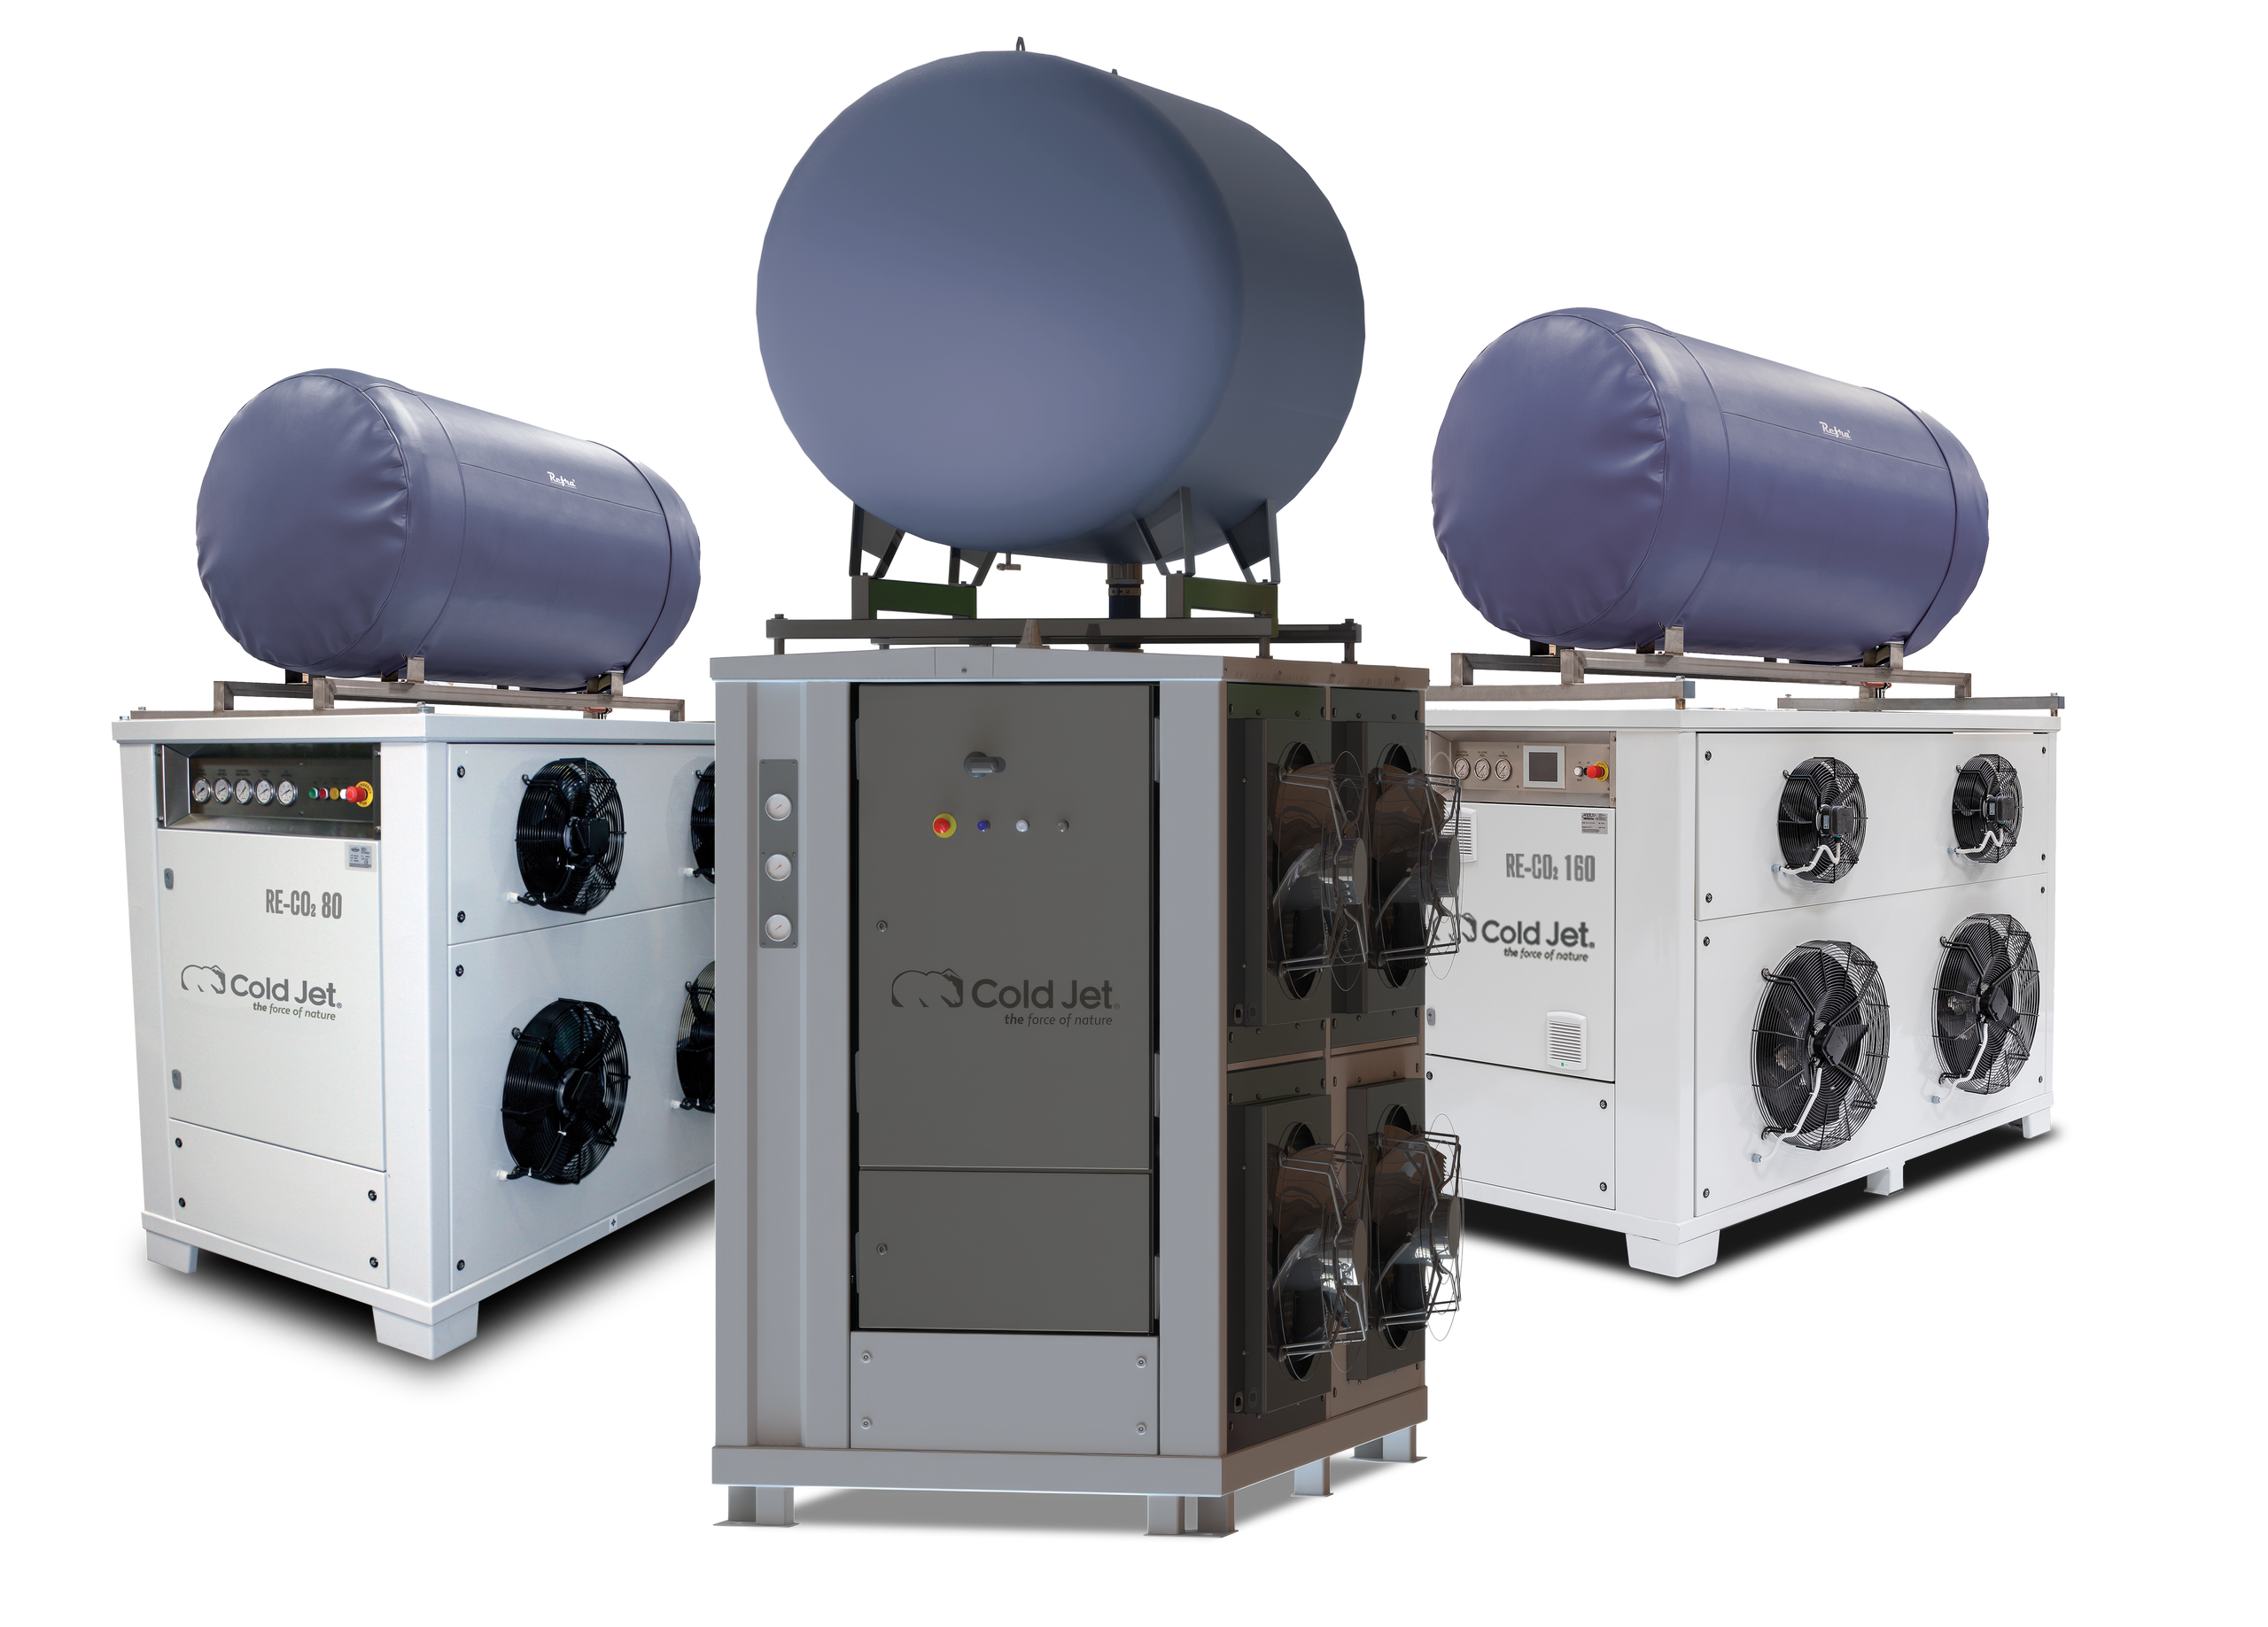
RE-CO2 320V2
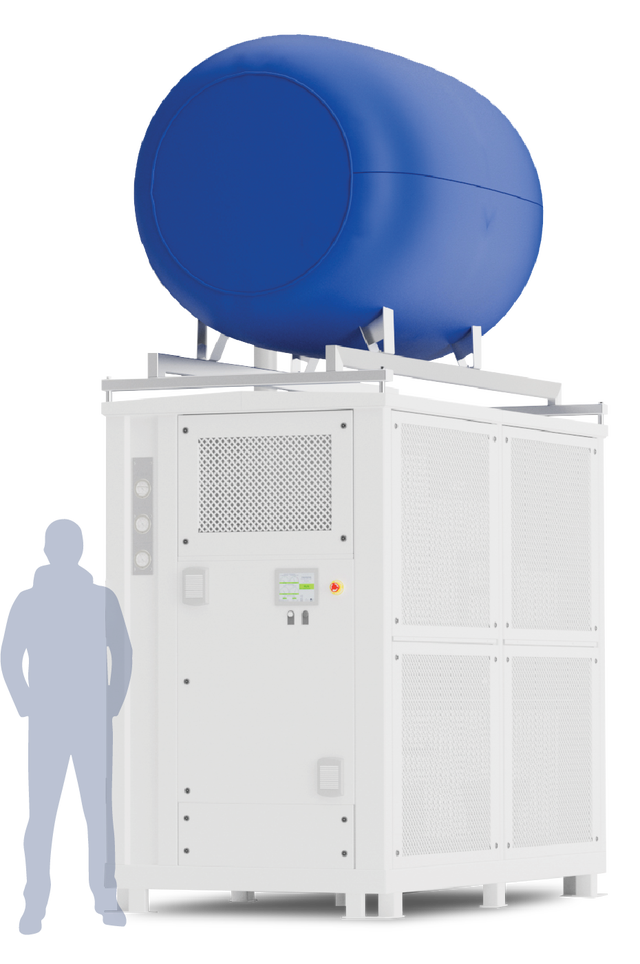
The most intelligent, scalable and sustainable CO₂ recovery system of its size. This compact unit captures pelletizer exhaust gas, reliquefies it and recycles it into more dry ice — and starts and runs directly from your Cold Jet pelletizer's control panel.
- Up to 320 kg/hr (705 lb/hr)
- 164 kWh per ton recovered
- Ideal for PR350H & PR750H
- Controlled from pelletizer HMI
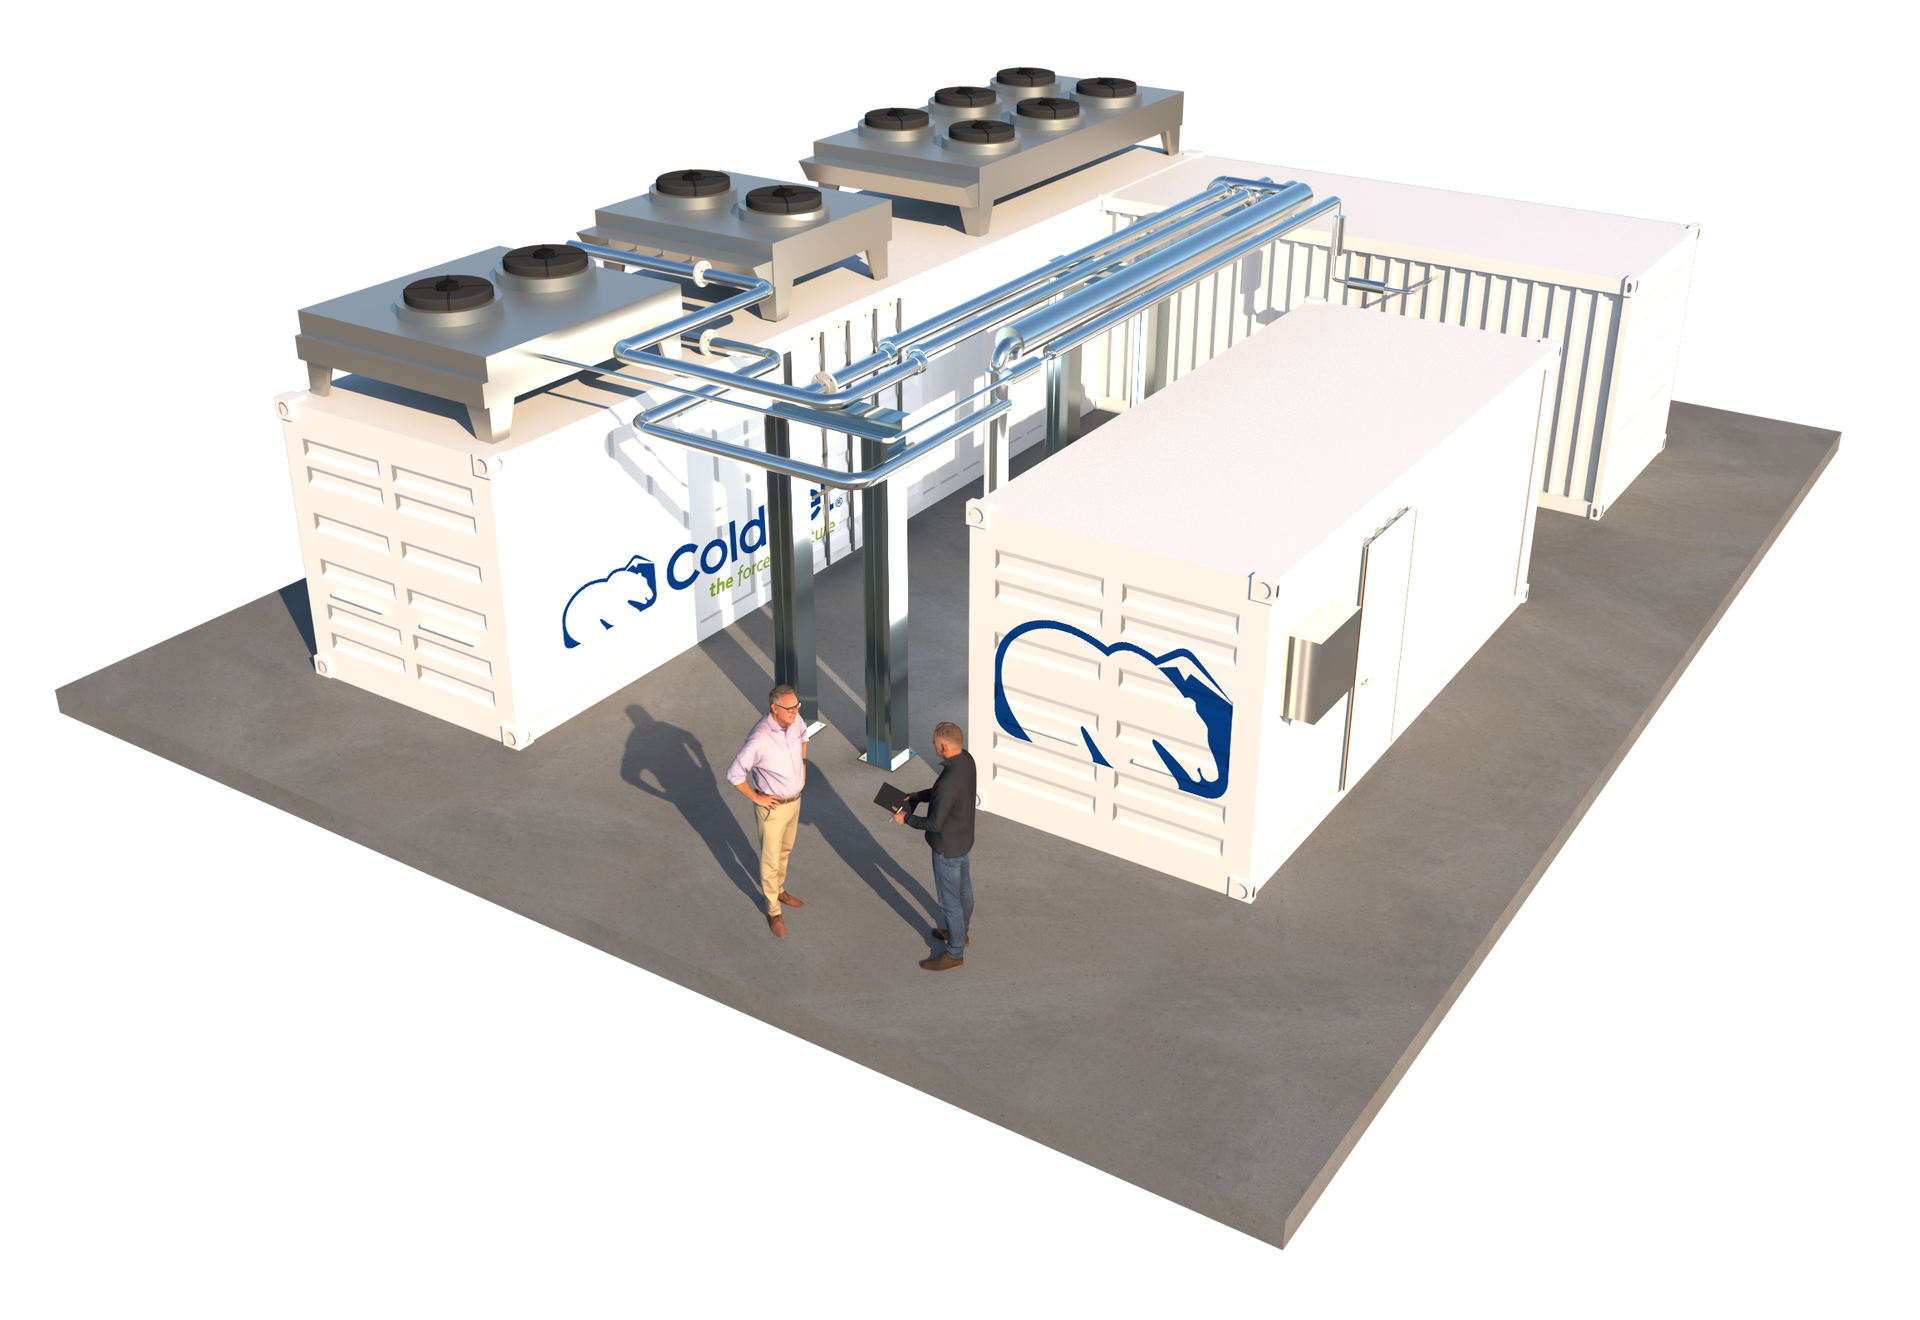
RE-CO2 3500
High-capacity recovery for plants running multiple PR750H pelletizers. Autonomous and containerized, it uses CO₂ (R744) as its refrigerant and has the lowest energy consumption per tonne recovered on the market.
- Up to 3,500 kg/hr (7,716 lb/hr)
- 135 kWh per ton recovered
- Containerized & fully autonomous
- CO₂ (R744) refrigerant
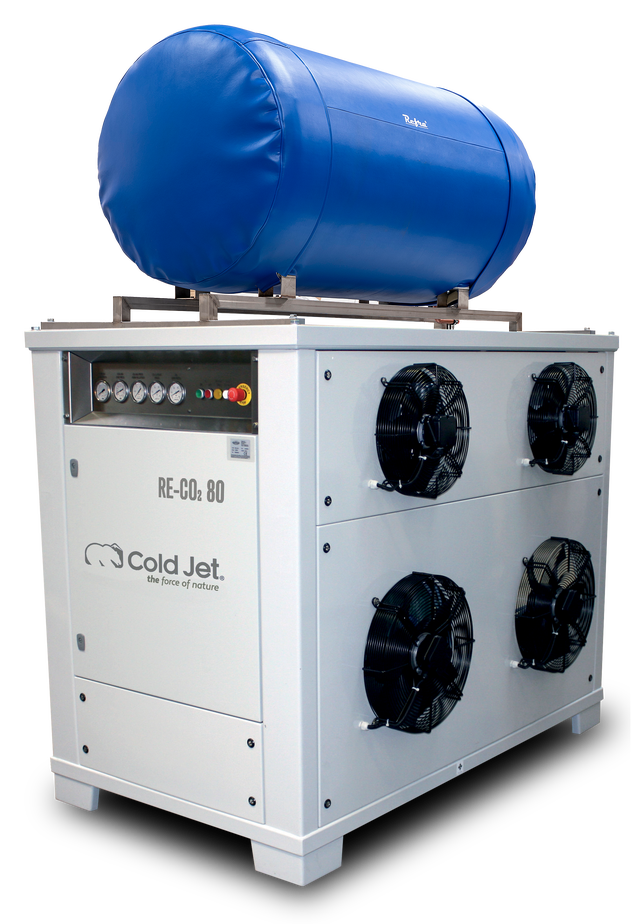
RE-CO2 80
The entry point for smaller dry ice operations. Pair it with a PE 80 pelletizer to start recovering vented CO₂ now, then scale up as efficiency and margins grow.
- Up to 80 kg/hr (176 lb/hr)
- 298 kWh per ton recovered
- Ideal for PE 80 pelletizers
- Modular, scalable design
Why Cold Jet
Why choose Cold Jet
for dry ice CO₂ recovery
Our recovery systems integrate with the pelletizers you already run, scale with your plant, and pay back quickly in liquid CO₂ savings.
Proven in dry ice plants worldwide
Dry ice producers including Carbon Capture Scotland, Soderal and Sutton-Garten already use Cold Jet recovery to raise profit, performance and production output.
Works with nearly any pelletizer
RE-CO2 systems integrate with all Cold Jet pelletizers and Integrated Blasting Systems, and are compatible with almost every other pelletizer brand on the market — no need to replace the equipment you already run.
Energy-efficient recovery
From 298 kWh per tonne recovered on the RE-CO2 80 down to 135 kWh per tonne on the RE-CO2 3500 — so the CO₂ you save isn't eaten up by energy costs.
Start small, scale up
A modular design and four capacities let you start with one unit and add more as savings grow, with intelligent gas-flow optimization across multiple RE-CO2 320V2 units.
Expert, custom-engineered solutions
Our experts configure each recovery system around your pelletizers, production volume and site, from standard units to custom platforms up to 5,000 kg/hr.
Our Customers
Dry ice producers trust Cold Jet for CO₂ recovery
Dry ice plants use Cold Jet RE-CO2 systems to increase profits, performance and production output.
See What Dry Ice Producers Are Saying About Cold Jet Equipment
We saw an immediate effect on our CO₂ ratio from 2.4:1 now to 1.35:1. Profit, production capability, and overall company performance is greatly improved.
Compliance
Supporting supplier rules, quality and sustainability
CO₂ recovery lets dry ice plants cut emissions and CO₂ purchases while respecting gas supplier rules and product quality.
Supplier Compliant
Gas supplier regulations
Gas companies strictly prohibit introducing external substances or recovered CO₂ back into their bulk liquid CO₂ tanks.
How We Comply
Recovered liquid CO₂ never enters the bulk tank — it is valved directly into the pelletizer feed line, keeping you compliant.
Same Quality
Dry ice quality
Any recovery process must keep the dry ice to the same standard your customers already rely on.
How We Comply
A closed-loop system eliminates the chance of contamination, so recovered CO₂ matches the quality of your liquid CO₂ supply.
Lower Emissions
Sustainability and ESG
Standard dry ice production vents roughly half of the liquid CO₂ it uses as exhaust gas to atmosphere.
How We Comply
Recovering and reusing that gas greatly reduces vented CO₂ and your carbon footprint, strengthening your ESG reporting.